Kerf Compensation for Laser Cutting: Measure and Test the Offset
Kerf compensation offsets the cutting path to account for material removed by the laser. Move an outside contour outward and a hole contour inward to retain more material. Under a symmetric-cut model, the per-edge offset is half the full kerf width. Establish the value for your setup, apply compensation once, and check dimensions separately from joint fit.
Published by: Laserlinez
Kerf compensation moves that path to allow for the material removed. Start with a drawing at the dimensions you want, establish an offset for your cutting setup, then check a small sample before committing to the full job.
Which way should the path move?
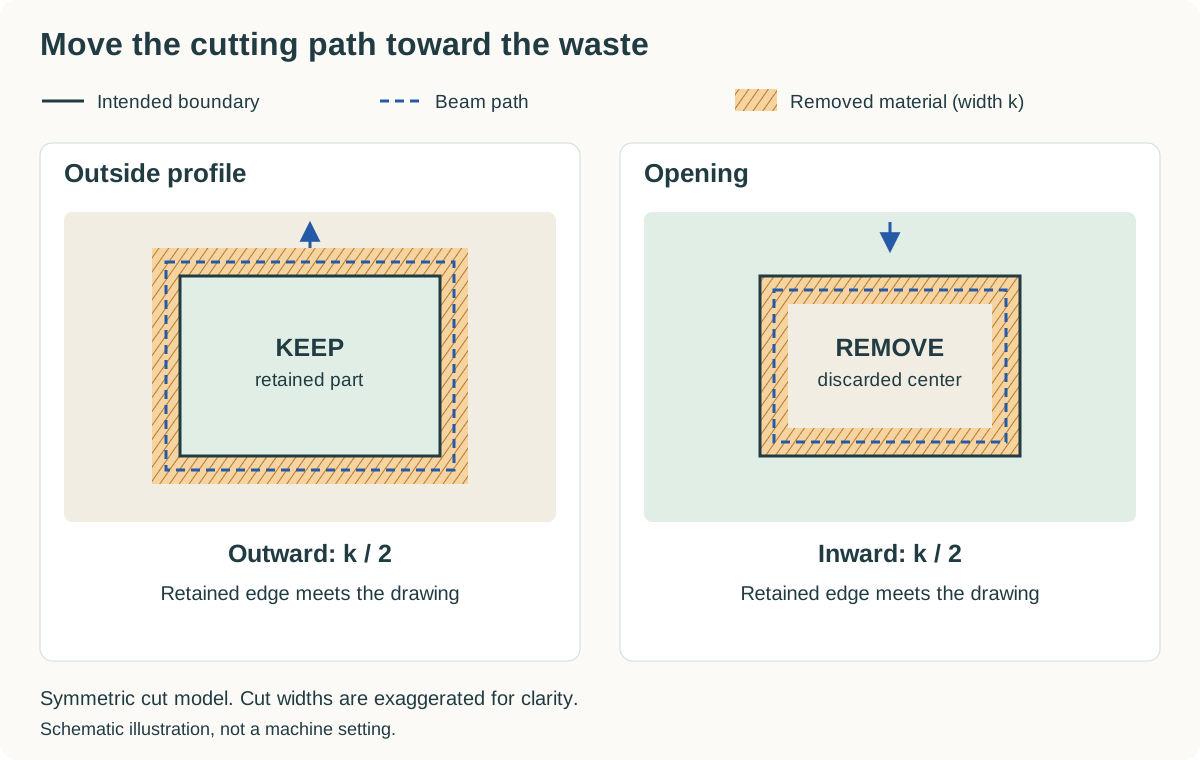
Think about the part you want to keep. For an outside profile, move the path outward, into the surrounding waste. For a hole or an internal slot, move it inward, into the piece that will be removed. In both cases, the purpose is to leave the retained material at the intended boundary.
In a simple model, the cut removes the same amount on each side of the beam's path. The required path offset is therefore half the kerf width. The actual cut still needs checking: an offset does not establish the machine's dimensional accuracy.
Calculate a starting offset
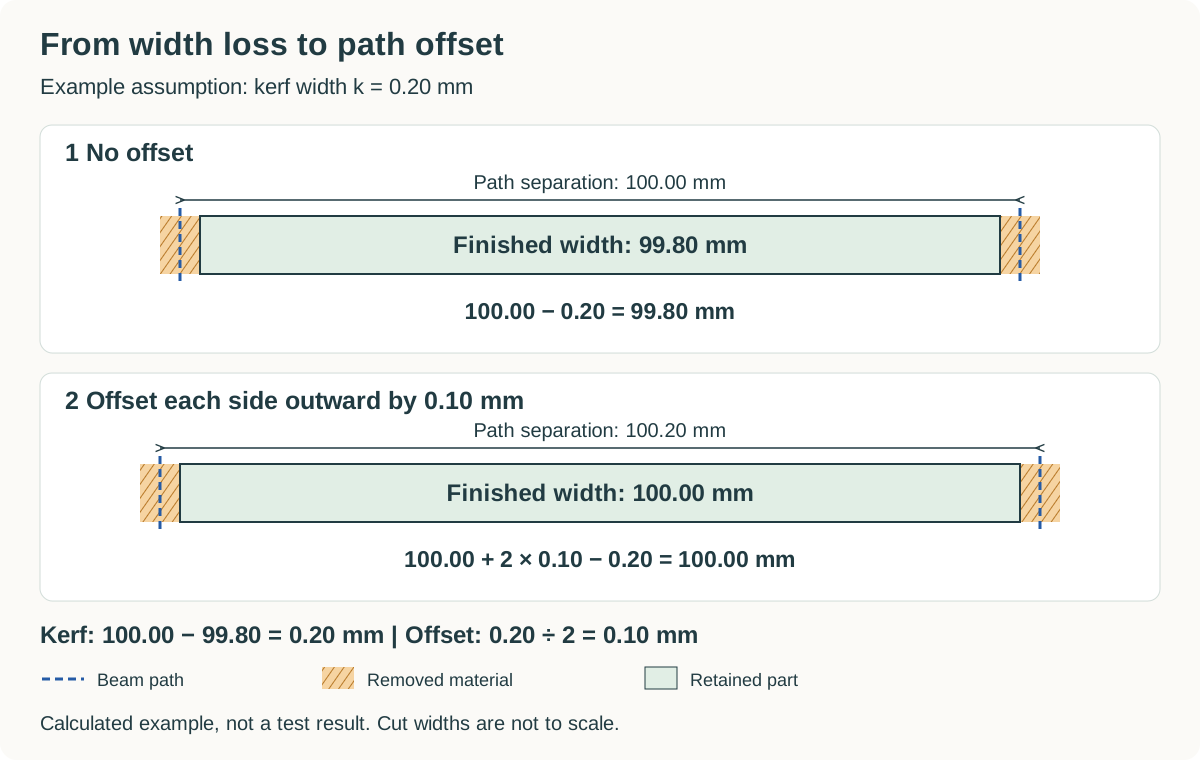
Suppose a square is drawn at 100.00 mm and, with compensation off, the finished piece measures 99.80 mm across one direction. Assume the file imported at the right size and the width difference comes from an even cut on both opposing edges.
- Estimated kerf
- 100.00 − 99.80 = 0.20 mm.
- Path offset
- 0.20 ÷ 2 = 0.10 mm outward.
Illustrative calculation under the stated assumptions, not a measured workshop result.
The measured width runs between two opposing edges. Each loses half the cut width, so the total width loss is one full kerf. The square's other two sides are not part of that measurement; do not divide the loss by four.
As a cross-check, moving both paths outward by 0.10 mm makes their separation 100.20 mm. Subtracting the assumed 0.20 mm kerf leaves a calculated finished width of 100.00 mm.
Establish a value for your setup
Use a spare piece of the material intended for the job, with the same thickness and finish. Start with cutting settings already suitable for that machine and material. An incomplete or inconsistent cut is a poor basis for compensation; address the cutting process first and follow the machine's operating instructions.
For a square measurement, check the imported dimensions and turn off any existing compensation. Cut the sample, measure its width in both directions, and compare a second sample before relying on the result. Record which direction each measurement describes. If the readings vary enough to change your offset choice, investigate that variation rather than treating one reading as definitive.
The calculation above is an estimate. Incorrect scale or machine calibration can also change the measured size. Correct those problems at their source; do not conceal them by adjusting kerf.
LightBurn provides a Vernier kerf test with instructions. Its procedure starts with Kerf Offset at 0 mm and its calculation returns the offset, not the full kerf width. Use that result as directed; do not halve it again. The linked file requires cutting and scoring settings appropriate to your setup.
Apply the offset in LightBurn
Set the offset
Put the intended closed contours on a Line layer. Open its Cut Settings Editor and set Kerf Offset, checking the units.
Check the direction
Positive values move a standalone contour outward; negative values move it inward. For nested contours on the same layer, LightBurn reverses the direction for the enclosed shape. Check a hole assigned to a separate layer independently.
Preview and test
Inspect Preview for the resulting path positions, including small openings and neighboring parts. Run a sample and compare its dimensions with the drawing.
LightBurn applies this offset to the output path without changing the original drawing. The documented feature requires closed shapes. See its Line Mode reference and kerf guide.
Apply compensation in one place. If the geometry has already been offset in a drawing program or supplied design, adding another offset can overcompensate. Keep an unchanged master and label any adjusted copy. Enlarging an entire drawing is not an equivalent fix: scaling also changes distances between features.
Check dimensions first, then the fit
A correctly sized tab and slot do not automatically make the joint you want. Compare the finished opening width with the corresponding width of the part it receives. Subtract the part width from the opening width: a positive result means clearance; a negative result means the part is wider than the opening. A joint that should slide apart needs a different allowance from one intended to grip. Decide what the assembly needs before changing the drawing.
For a tab and matching slot whose widths are both laser-cut, retaining more material makes the tab wider and the slot narrower. That reduces clearance. Retaining less material increases clearance. Increasing the offset outward on the tab and inward on the slot leaves more material and can therefore make an already tight joint worse.
If the individual dimensions match the drawing but the fit is wrong, adjust the intended clearance in the design. If the dimensions are wrong, check the compensation and cutting consistency first. Change one thing at a time so the next sample tells you which change helped.
A slot that receives the edge of another sheet is a different case: it must accommodate that sheet's actual thickness, which a path offset cannot change. Correct the relevant design dimensions when the stock differs from the drawing. LightBurn's Resize Slots & Tabs documentation describes a separate tool for supported geometries.
If the result still does not match
- Both the size and feature spacing are wrong: check units and import scale before changing compensation.
- One direction fits differently from the other: compare the two measured directions. LightBurn documents direction-dependent kerf for some non-circular beams; one offset may not suit both axes. Beam-shape guidance.
- An opening disappears or paths overlap: inspect the offset in the preview and revise the geometry or spacing before cutting.
- A setting worked on another job: confirm the material, thickness, cutting conditions, and any existing design allowance before reusing it.
- A compensated sample is too tight: measure the pieces and check for double compensation before increasing any value.
Before cutting the final parts
- Confirm the imported size and units.
- Confirm which outlines define retained parts and which define openings.
- Apply compensation once and inspect the resulting paths.
- Check a sample for the dimensions and fit the job needs.
- Save the drawing and a job note together: material, measured thickness, machine, cutting settings with units, offset, orientation, and sample result.
Common questions
Do not use it as a substitute for checking the cut. A spot specification describes the beam; the value needed here describes material removed by your cutting process. Establish the offset from a suitable sample or a documented test.
Consider the required dimensions and fit. A decorative outline may tolerate the small difference; an opening for another component may not. There is no single acceptable tolerance for all projects.
Follow that service's instructions. For example, SendCutSend asks for the intended dimensions and handles kerf itself. Confirm the receiving workflow before modifying the geometry.
Preparing the vector file
If your starting point is a bitmap logo or silhouette, Laserlinez Contour Vectorization can help create vector boundaries. Check their dimensions and suitability for the part. Kerf measurement, allowances, and machine settings still belong to the cutting workflow.
Documentation
Documentation checked on 26 September 2026. English LightBurn control names are used to identify the referenced settings.
Comments
Loading comments...